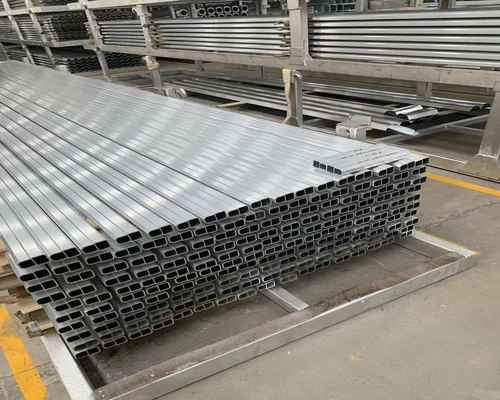
Structural and hollow sections
Multi-void sections with balanced walls, designed so the die fills evenly and the profile stays straight through the run.
Frames, beams, battery housingsRaw Materials · Aluminum Products
A custom profile starts with a die, and the die starts with a drawing that respects how aluminum flows. Wall balance, corner radii and the circumscribed circle decide whether the section extrudes cleanly or warps through the whole run.
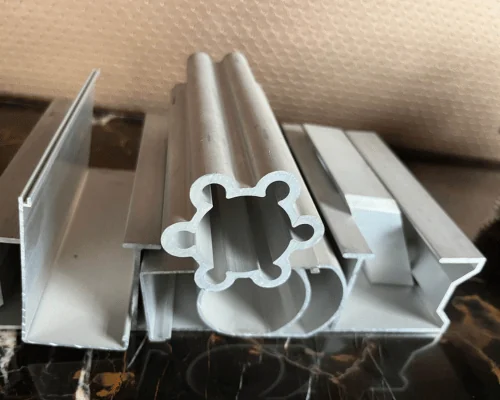
Four routes cover most of what we quote. Each is a different mill or process route, so the size window and the lead time differ even where the grade looks similar.
Multi-void sections with balanced walls, designed so the die fills evenly and the profile stays straight through the run.
Frames, beams, battery housings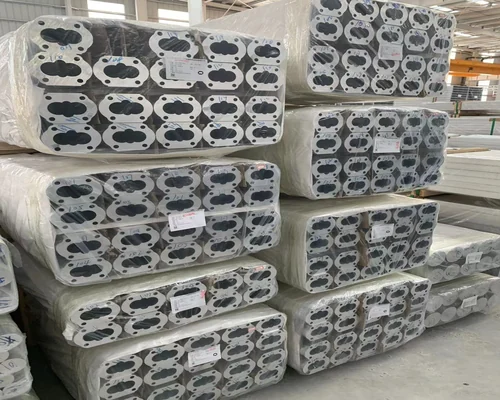
Fins extruded as part of the section, with the fin spacing and root thickness set by the die rather than by a later machining step.
Electronics cooling, LED luminaires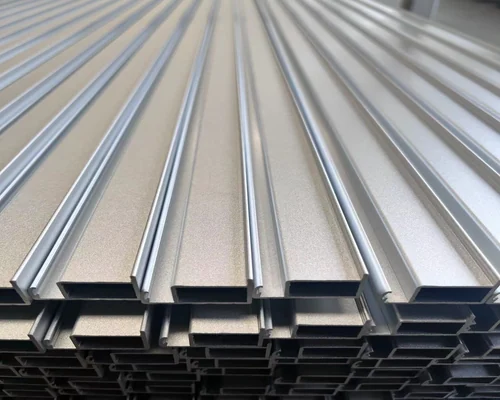
Purpose-made mullions, trims and handrails that have to meet an existing building or product detail.
Facades, interiors, shopfitting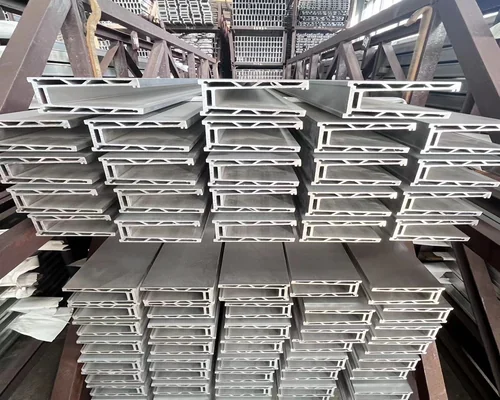
Extrusion plus CNC drilling, tapping, bending and anodizing, supplied as a finished part rather than a length of metal.
Automation parts, enclosures, transportCustom extrusion is quoted from the drawing plus the quantity. Tooling is a one-off cost, and the per-metre price falls as the run gets longer, so the two are always quoted together.
Swipe the table sideways for the notes →
| Parameter | Range | What decides it |
|---|---|---|
| Profile weight | From roughly 0.2 kg/m upwards | Weight per metre drives the press size and the price per metre. |
| Circumscribed circle | Up to the press capacity, confirmed per section | A section that does not fit the container cannot be extruded at any price. |
| Alloys | 6063, 6061, 6082, 6005, 7005 | Strength, finish and weldability trade off against each other in the alloy choice. |
| Temper | T4, T5, T6 | T6 for machined and loaded parts; T5 for architectural and frame sections. |
| Length | Cut to length from the extrusion run | Cutting after ageing avoids marking the finished surface. |
| Finishes | Anodized (clear or colour), powder coated, electrophoresis | Deep colour anodizing needs a tighter alloy and a better surface than clear. |
What separates a good custom extrusion from a difficult one is decided on the drawing, before any aluminum is heated.
A section with one thick wall and one thin wall cools unevenly and twists. Balanced walls extrude straight and hold tolerance.
Sharp internal corners and long thin tongues wear the die and limit the run length. Rounded corners cost nothing and last.
That changes tooling cost and the achievable wall. It is a design decision with a price attached, not a manufacturing detail.
Deep anodizing colours need a tighter chemistry and a better surface finish; specifying the colour after choosing the alloy can force a change.
Custom profiles are quoted from a drawing and a quantity. These are the four points we settle before the die is ordered.
Dimensions, wall, radii and the tolerance class. A DXF or a dimensioned PDF is enough to review.
6063-T5 for architectural, 6061-T6 for structural or machined parts, 6082 where strength and anodizing quality both matter.
Tooling is quoted once; the per-metre price depends on the total quantity, so the two are decided together.
Machining, bending and the finish are scheduled in that order, so nothing is cut or drilled after anodizing.
Custom extrusions turn up wherever a standard section is close but not right, and the difference is worth a die.
Finned and hollow sections where the geometry is the function and a standard profile cannot carry it.
Structural sections in 6061 or 6082, extruded, machined and anodized as a finished part.
Purpose-made mullions, trims and handrails that have to meet an existing building detail.
Frames with integrated cable channels, mounting faces and locating features that would otherwise need welding.
Have a section drawing that needs a die quote? Send the specification, quantity and any certification requirement and we will come back with what we can supply.
Get Instant Quote