SHBD Metal produces custom zinc die castings in Zamak 3, 5 and 7 and ZA-8 — thin-wall parts with sections down to 0.8 mm, as-cast tolerances to ±0.01 mm and tool life beyond 1,000,000 shots. Send a 3D model for an instant quote, from prototype validation to high-volume production.
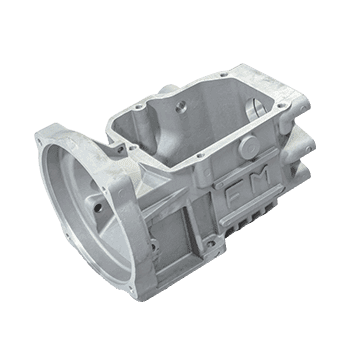
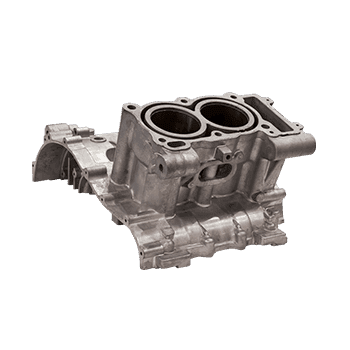
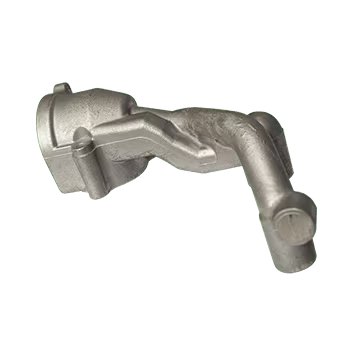
Get instant pricing, project lead times, and DFM feedback for your zinc part.
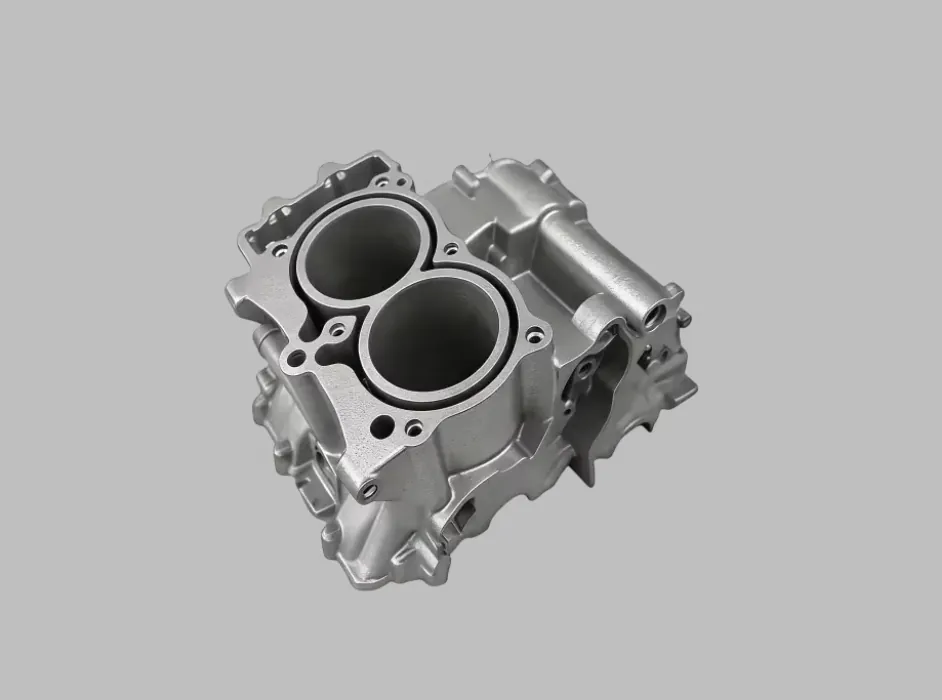
Zinc die casting is a high-volume process that injects molten zinc alloy — most often Zamak 3, 5 or 7, or ZA-8 — into a hardened steel die. Zinc alloys are cast on hot-chamber machines, where the metal is melted inside the machine and injected in very short cycles, which is why zinc delivers the highest production rates of any die casting process and tool life beyond 1,000,000 shots.
The fluidity of zinc alloys allows walls as thin as 0.8 mm, fine detail, tight as-cast tolerances (±0.01 mm on critical features) and near-net shapes that need little or no machining. Zinc castings are also the easiest die castings to plate and finish, which is why they dominate decorative and functional hardware.
SHBD Metal handles the full chain in-house: DFM review and mold flow analysis, tooling in premium hot-work steel, die casting, secondary CNC machining, surface finishing and dimensional inspection. Send a 3D model to get a quote with manufacturability feedback.
Get Instant QuoteFrom small plated hardware to functional housings and brackets, we manufacture zinc parts with tooling, machining and finishing managed in-house. Upload a model to receive an instant quote and manufacturability feedback.
Zinc alloys run on hot-chamber machines with cycle times a fraction of cold-chamber aluminum, which suits volume production of small to medium parts with very long mold life.
Get a Quote
Sections down to 0.8 mm, moulded-in threads, bosses and fine surface detail — the geometry that makes zinc the standard choice for connectors, locks, hinges and precision hardware.
Get a Quote
We help you choose Zamak 3, 5 or 7 and ZA-8 by strength, hardness, plating response, creep resistance and cost, and we document the alloy lot on every shipment.
Get a Quote
Trimming, drilling, tapping, CNC machining, tumbling, chromate passivation, chrome and nickel plating, powder coating and painting — all co-ordinated on one project.
Get a Quote
| Capability | Details |
|---|---|
| Dimensional Tolerance | Critical features hold ±0.01 mm as cast, which minimizes secondary machining and ensures precision fit in assemblies. |
| Minimum Wall Thickness | Zinc alloys: 0.8 mm. Zinc's high fluidity allows very thin sections, provided the wall thickness stays uniform and gates are designed for it. |
| Wall Thickness Uniformity | Keep transitions within a 1:3 ratio to prevent warpage, sinks and internal stress, so part quality stays consistent across the run. |
| Hole Diameter & Threading | Holes under 3 mm in diameter and all threaded features are produced by secondary CNC machining for reliable precision and thread quality. |
| Draft Angle | A minimum 0.5° draft angle is recommended for clean ejection, good surface quality and longer mold life. |
| Maximum Mold Life (Cycles) | Zinc: 1,000,000+ cycles — roughly ten times the tool life of an aluminum die casting mold (100,000+ cycles), which lowers tooling cost per part at volume. |
| Minimum Order Quantity (MOQ) | Flexible order volumes from 500-1,000 pieces, suitable for prototype validation and mid-volume production. |
| Standard Lead Time | 20-25 days for the production mold and first parts. The timeline is confirmed against final part complexity and tooling requirements. |
Zinc and aluminum are the two die casting alloys we cast most often. The choice usually comes down to wall thickness, part size, weight and how the part will be finished.
| Aspect | Zinc | Aluminum |
|---|---|---|
| Min. wall thickness | 0.8 mm | 1.5 mm |
| Density | ≈6.6 g/cm³ (Zamak) | ≈2.7 g/cm³ |
| Casting temperature | ≈400-420 °C | ≈650-700 °C |
| Machine type | Hot chamber | Cold chamber |
| Mold life | 1,000,000+ shots | 100,000+ shots |
| Typical part size | Small to medium, intricate | Medium to large, structural |
| Weight for same volume | Heavier | About 2.5× lighter |
| Finishing strength | Chrome, nickel and brass plating; chromate passivation | Anodizing and chromate conversion |
| Best when | Thin walls, fine detail, high volume, plated finish | Larger parts or weight saving comes first |
Zinc parts are cast from Zamak and ZA alloys on hot-chamber machines, and the tooling is cut from hardened hot-work steel. No other die casting alloy accepts such a wide range of decorative and protective finishes.
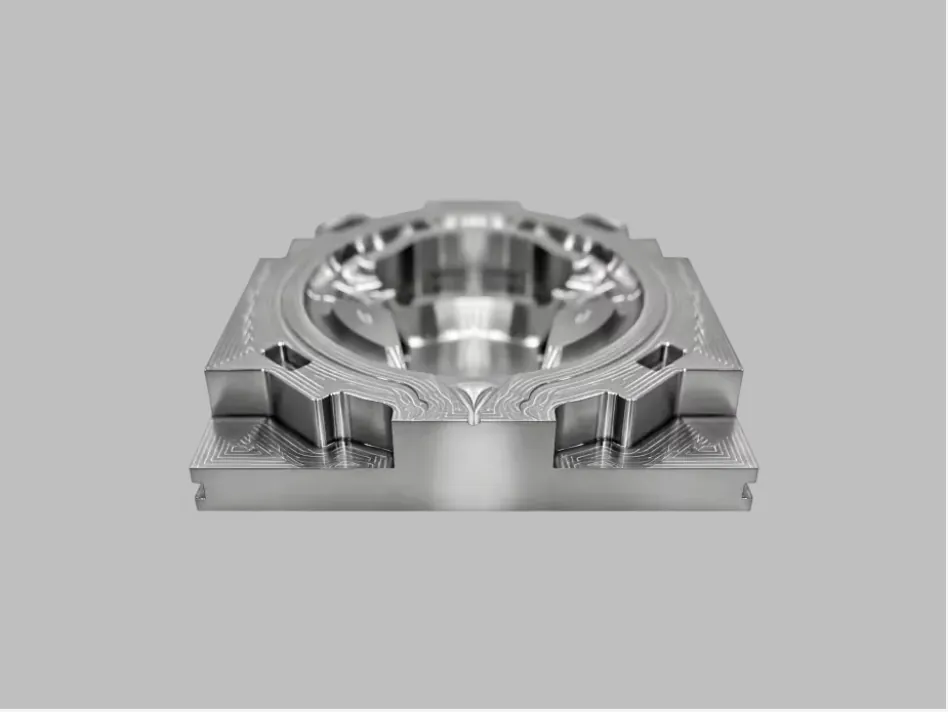
Excellent high-temperature strength and toughness. Resists thermal cracking and maintains hardness under prolonged heat exposure. The ideal choice for aluminum and zinc die casting molds requiring durability and precision.
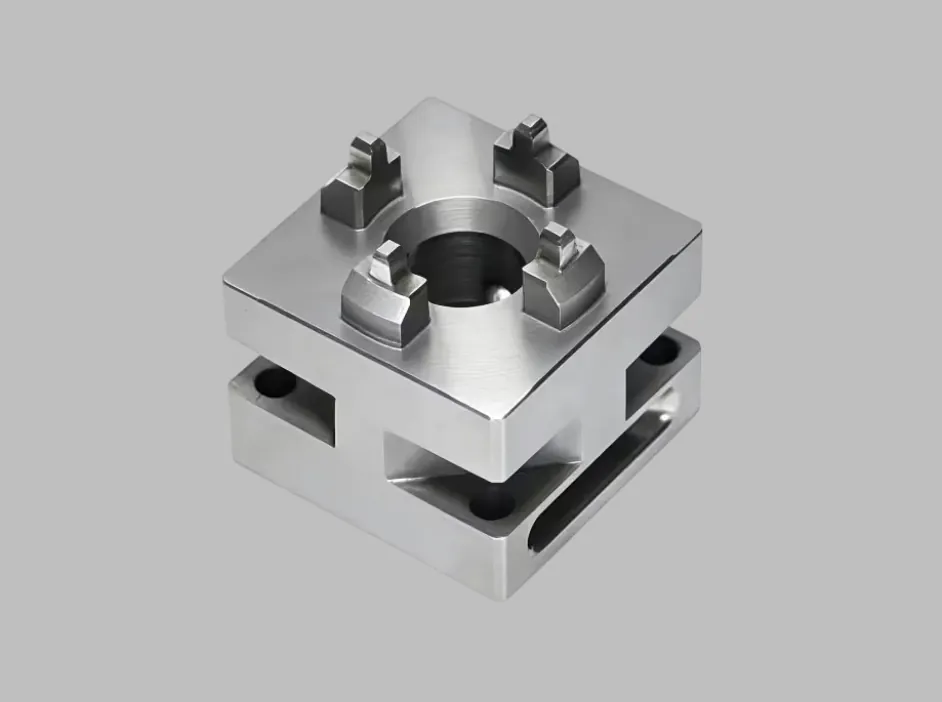
DIN 1.2344 premium hot-work tool steel offering excellent high-temperature strength and superior thermal fatigue resistance. A dependable choice for aluminum and zinc die casting molds operating under intense thermal cycling.
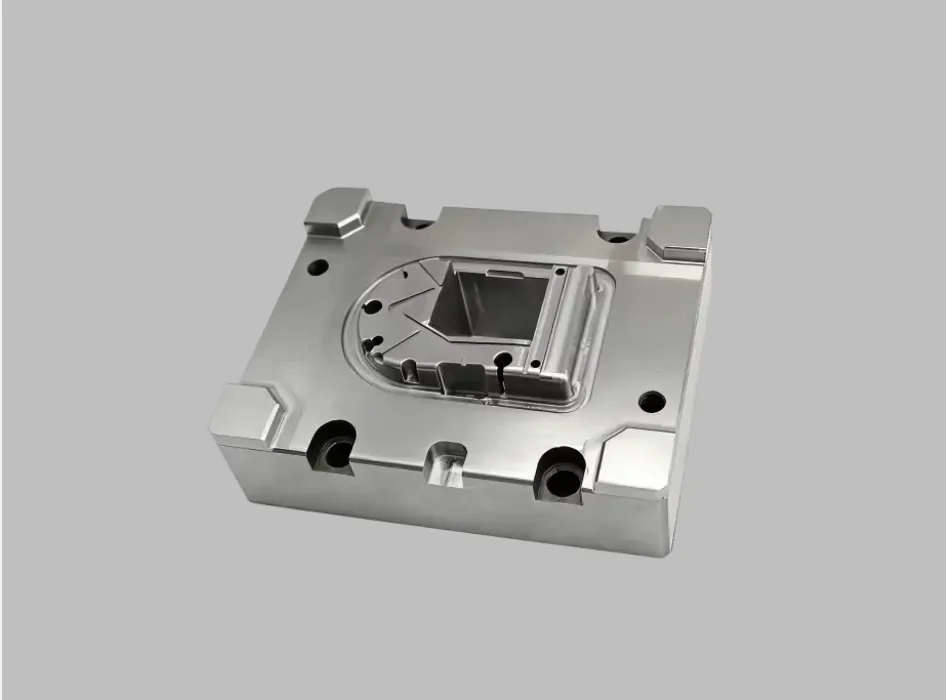
Premium hot-work die steel with exceptional impact toughness and thermal conductivity. Extends mold life under severe thermal cycling while maintaining hardness and dimensional stability for long-run production.
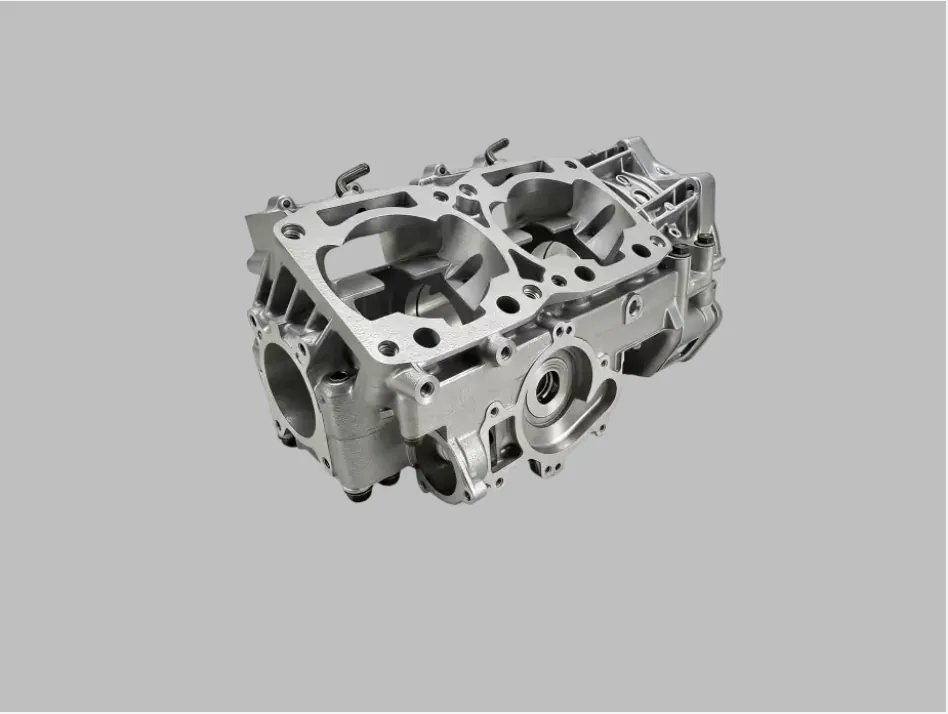
Lightweight, corrosion-resistant, excellent strength-to-weight ratio and thermal conductivity. Ideal for complex, thin-walled components in automotive, aerospace, and electronics.
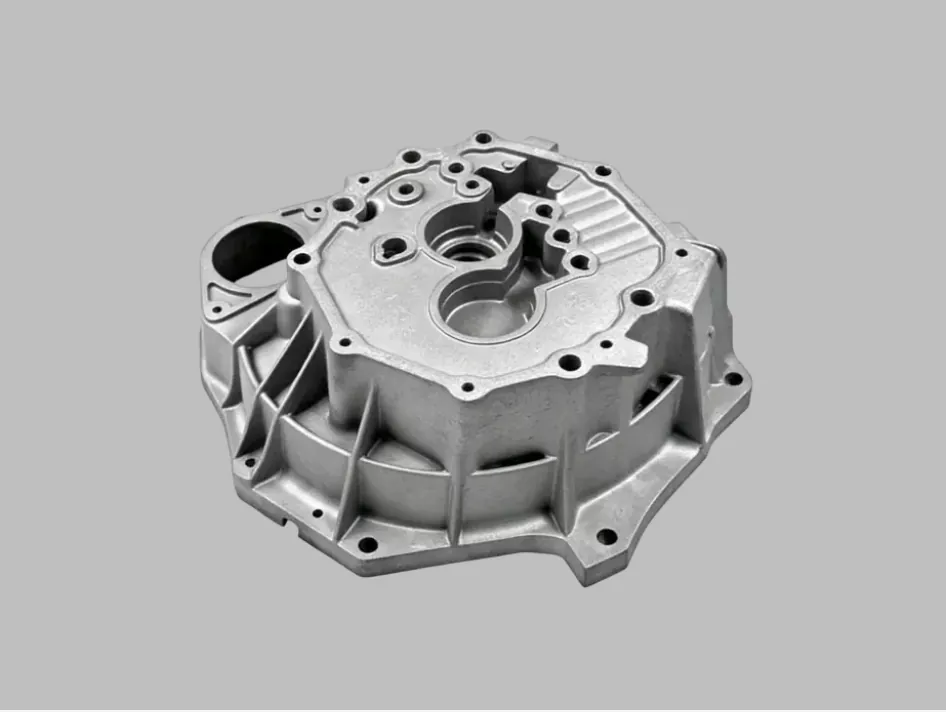
Exceptionally lightweight with excellent dimensional stability and EMI/RFI shielding capability. Magnesium alloys are ideal for portable electronics, automotive, and weight-critical applications without sacrificing strength.
Superior fluidity enables extremely thin walls and intricate geometries. Zinc alloys offer excellent plating and finishing characteristics, high impact strength, and mold life up to 1,000,000 cycles — ideal for hardware, decorative, and precision components. See our zinc die casting services for alloys, wall thicknesses and lead times.
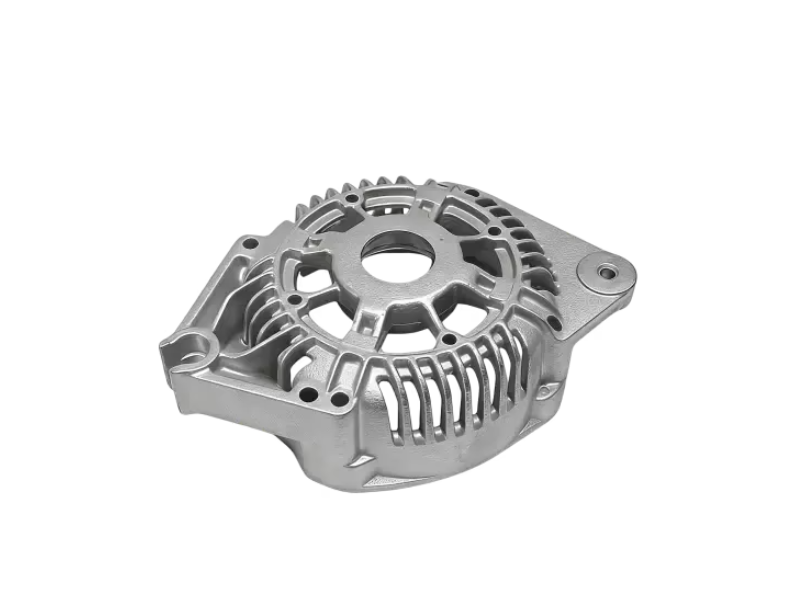
The standard finish straight from the die. It provides a functional surface that is cost-effective, suitable for non-visible components or as a base for secondary finishing operations.
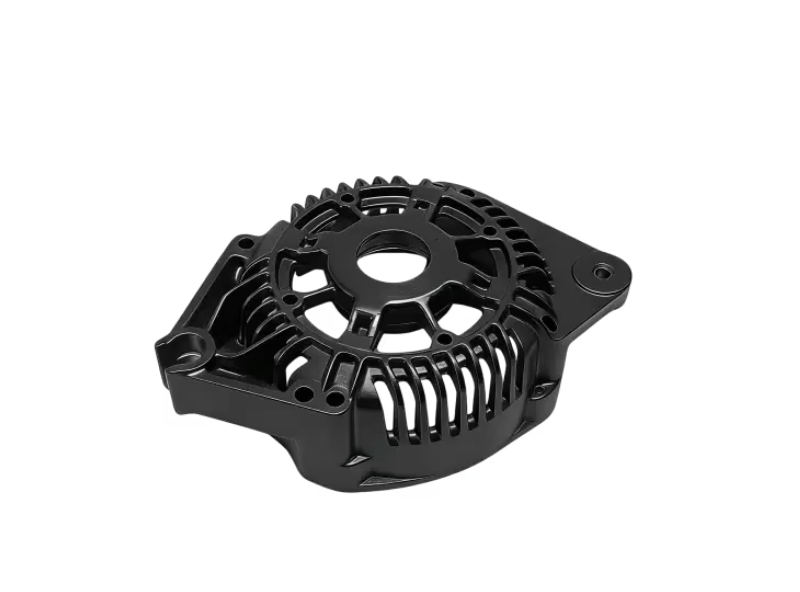
An electrochemical process primarily for aluminum that enhances surface hardness and corrosion resistance. It creates a porous oxide layer that can be dyed in various colors for improved aesthetics and part identification.
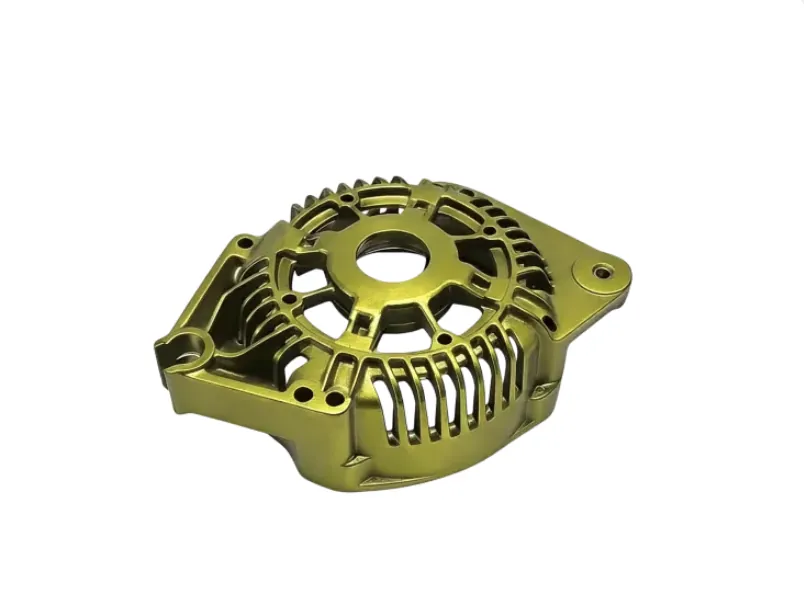
A chemical conversion coating for aluminum and zinc alloys that significantly improves corrosion resistance. It creates a conductive surface ideal as a pretreatment for painting or as a final finish with a distinctive iridescent yellow-green color.
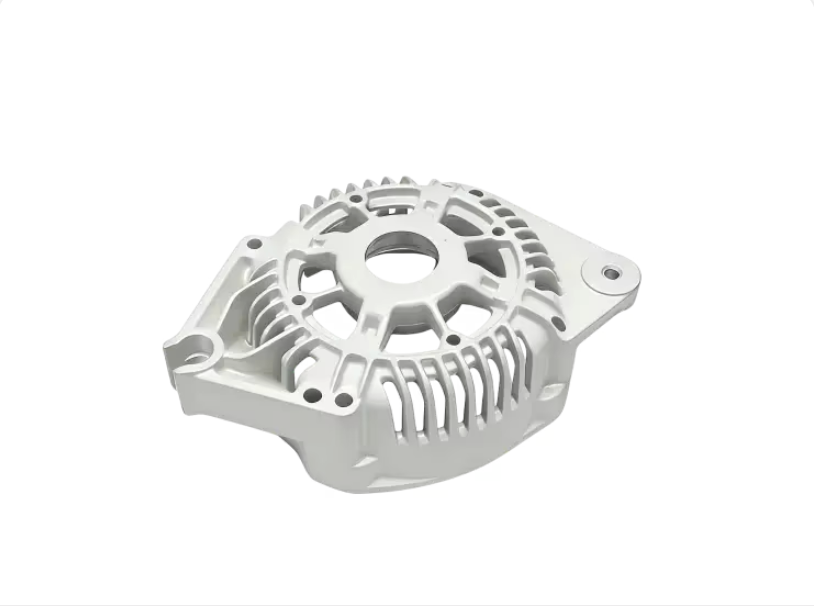
A dry finishing process where electrostatically charged powder is applied and cured into a hard, durable layer. It provides excellent corrosion and wear resistance, a uniform appearance, and is available in a wide range of colors and textures.
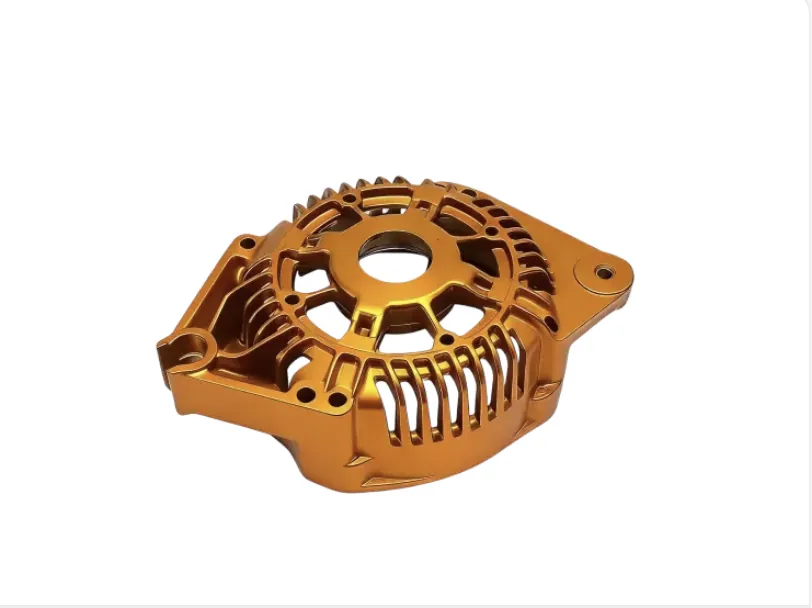
Applies wet liquid coatings (e.g., enamel, acrylic) to add color and enhance visual appeal. It offers additional protection against corrosion and UV exposure, commonly used for branding and meeting specific environmental or color-matching requirements.
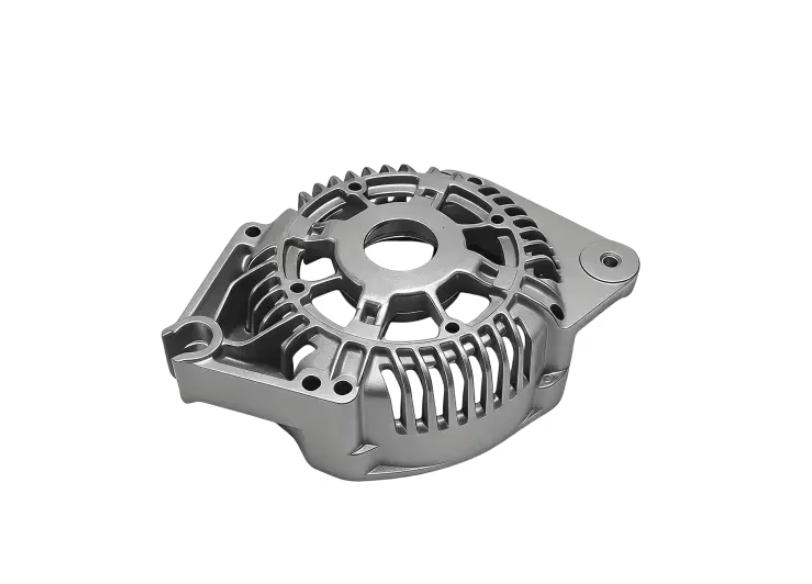
A mechanical process that propels abrasive media to clean, texture, or deburr surfaces. It produces a uniform matte finish, removes minor imperfections, and enhances the adhesion of subsequent paint or coating layers.
Zinc castings are frequently machined after casting to add threads, sealing faces, bearing bores and features that are impractical to mould. Our engineering team reviews the casting and the finished drawing together so the machining strategy holds critical tolerances without adding unnecessary operations.
High-Precision CNC Machining: Multi-axis milling and turning to hold tight tolerances and create precise mounting features, threads, and sealing surfaces.
Wire EDM (Electrical Discharge Machining): For producing intricate contours, sharp internal corners, and fine details that are challenging for conventional cutting tools.
Secondary Finishing & Inspection: Comprehensive services including deburring, surface treatment, and final CMM inspection to guarantee quality and readiness for assembly.
Learn More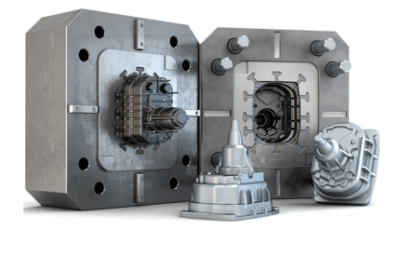
SHBD Metal integrates quality control into every step of zinc production — alloy verification, process monitoring and dimensional inspection — so parts stay reliable across the whole run.
Spectrometer testing guarantees alloy conformity and batch consistency.
CMM and optical scanning maintain tolerances within ±0.005mm.
Automated vision systems detect imperfections and finish defects.
X-ray and ultrasonic testing identify porosity and structural flaws.
Hardness and tensile testing verify strength and durability.
Pressure tightness and leak tests under simulated conditions.
Uniform thickness measurement for corrosion protection.
PPAP reports and material certifications for every batch.
We employ industry-leading metrology equipment for rigorous validation. Spectrometers verify alloy chemistry, while high-precision CMMs and 3D optical scanners inspect complex geometries. Dedicated instruments for surface finish, thread gauges, and automated vision systems ensure every critical dimension and feature meets specification.
Every component undergoes a multi-stage verification protocol: material certification, mechanical property testing, corrosion resistance validation, and functional performance checks (e.g., pressure tightness). This holistic approach guarantees your parts perform reliably in their intended application and environment.
Our process yields a first-article inspection pass rate exceeding 95%. We stand behind this reliability with a quality guarantee: should any part fail to meet agreed specifications, we will remake it at no cost. Final audit inspection is mandatory prior to every shipment.
Experience our precision-driven quality system. Submit your design for a detailed quote and see the difference rigorous control makes.
Start Your Die Casting ProjectSHBD Metal produces zinc components for applications where thin walls, dimensional stability, plating quality and long production runs decide the unit cost.
Locks, handles, brackets, sensor housings, connectors and charging hardware where thin walls, strength and a plated finish matter.
Connector shells, shielding housings and small enclosures that need fine detail, dimensional stability and a platable surface.
Door and window hardware, hinges, locks and fittings cast, machined and plated in production volumes.
Brackets, housings, levers and fittings engineered to hold up under vibration and repeated service loads.
Corrosion-resistant fittings, terminals and metering housings for power distribution equipment.
Instrument housings and components cast with full material traceability under our ISO 9001:2015 quality system.
Explore more manufacturing capabilities from SHBD Metal.